Explore our benchmark private label products manufactured under validated EU quality controls, high bioavailability standards, and scalable batch capacities.
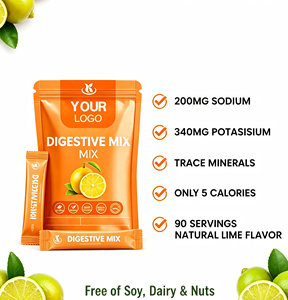
Navigating global dietary supplement manufacturing requires deep technical scrutiny of compliance frameworks, analytical capabilities, bioavailability engineering, and supply chain integrity.
The global nutraceutical marketplace has transitioned from basic ingredient blending to a highly sophisticated science-driven sector. Brand owners, clinical nutrition companies, and international distributors can no longer rely on superficial manufacturer claims. Establishing a resilient supply chain demands partnering with top trusted nutritional supplements factories that operate under strict international regulatory standards, including European Union GMP (Good Manufacturing Practice), ISO 22000 Food Safety Management Systems, and HACCP (Hazard Analysis Critical Control Point) controls.
Contract manufacturing facilities servicing modern wellness brands must enforce stringent quality assurance (QA) and quality control (QC) workflows across every step of production:
Flexible operational models designed to scale alongside your brand from early-stage market testing to high-volume retail distribution.
Accelerate time-to-market with production-proven, shelf-ready formulations. Ideal for brands seeking low minimum order quantities (MOQs from 500 units) with fully compliant, customized packaging, label design, and analytical support.
Engineered proprietary nutrient matrices developed by senior biochemical scientists. From synergistic adaptogen complexes to micro-encapsulated vitamins, we turn intellectual concepts into scalable commercial reality.
High-volume continuous output for established brands. Automated two-piece capsule filling, tablet compression, liquid filling, multi-head powder pouching, and functional protein bar extrusion operating under strict cGMP protocols.
Analyzing key market shifts, formulation advancements, and procurement evolution shaping the next decade of nutraceutical manufacturing.
Traditional hard-shell capsules and plain tablets are rapidly yielding market share to novel, sensory-rich, and targeted delivery formats. Modern B2B buyers are prioritizing:
Procurement teams are restructuring vendor evaluations around environmental stewardship and verified ingredient provenance:
Direct technical answers to common questions raised by brand managers, compliance officers, and procurement specialists during factory evaluation.
For ready-to-brand stock formulations (such as standard vitamin capsules, electrolyte powders, or botanical extracts), MOQs start as low as 500 bottles per SKU. Custom ODM formulations, specialized gummy confections, complex powder blending projects, or custom-extruded protein bars typically start from 2,000 to 5,000 units, dictated by raw material MOQs and specialized line setup requirements.
We execute a fully documented Quality Management System (QMS). Every incoming raw material undergoes FTIR identity verification and microbiological/heavy metal clearance. Standard Operating Procedures (SOPs) mandate continuous in-process checks (tablet hardness, capsule weight variation, seal integrity, and moisture activity $a_w$). Every finished batch is issued a comprehensive Certificate of Analysis (CoA) linked to retained reference samples stored for the duration of shelf life.
For stock private label items with approved customer artwork, typical manufacturing turnaround is 3 to 4 weeks. Custom formulation projects requiring specialized ingredient sourcing, flavor matching, pilot stability testing, and packaging customization typically require 6 to 8 weeks from final specification lock to pallet release.
Yes. Our regulatory services team conducts ingredient safety audits against EU Novel Food catalogues, validates dosage thresholds against international health authority guidelines, and reviews packaging layout text to ensure full compliance with Regulation (EU) No 1169/2011 (Food Information to Consumers) and Regulation (EC) No 1924/2006 (Nutrition and Health Claims).
We provide a wide array of packaging formats including recyclable PET and HDPE bottles, amber glass jars, blister packs, single-serve sachets, aluminum-lined resealable stand-up doypacks, and bulk drums. We also offer sustainable post-consumer recycled (PCR) plastics and compostable flexible films upon request.
Whether you require fast-track private label dispatch or custom scientific formulation, our engineering team is ready to scale your product line safely and efficiently.
Inquire Now