The global market for metabolic health supplements is experiencing a profound paradigm shift. Driven by rising consumer awareness surrounding mitochondrial efficiency, glucose homeostasis, cellular energy production (ATP), and metabolic flexibility, brands require robust, highly compliant, and technically advanced manufacturing partners. Navigating international supply chains requires working with top-tier, trusted metabolic support factories that guarantee absolute ingredient purity, precise active-compound assays, and complete analytical traceability.
This comprehensive industry whitepaper evaluates key formulation archetypes, contract manufacturing capabilities, quality control benchmarks, and future procurement vectors. Operating from cleanroom-certified facilities in Varna, Bulgaria, compliant with EU Food Safety Management Systems (HACCP), ISO 22000, and Good Manufacturing Practice (GMP), our manufacturing infrastructure offers brand owners a competitive advantage through lower operational friction, rigorous scientific backing, and rapid market deployment.
Production-ready, scientifically optimized, and fully customizable for private label execution
Translating clinical research into stable, bioavailable contract manufacturing solutions
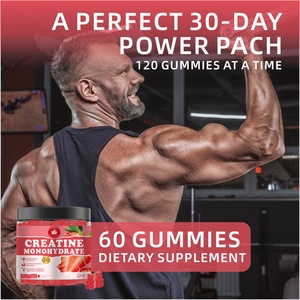
Creatine monohydrate remains the gold standard in cellular energy modulation. By increasing phosphocreatine stores within skeletal muscle and neural tissue, it accelerates ADP-to-ATP recycling via the creatine kinase pathway.
Our factory specializes in 200-mesh micronization, ensuring complete solubility and reduced gastrointestinal distress. Furthermore, our proprietary gummy thermal-processing technology protects the heat-sensitive creatine molecule from degrading into creatinine during confectionery cooling.
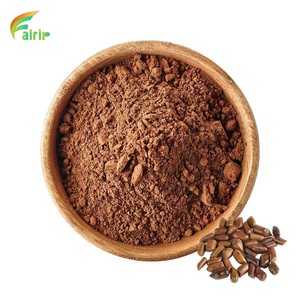
Botanical compounds such as Cassia Seed Extract (10:1) and Berberine HCl act directly upon Adenosine Monophosphate-Activated Protein Kinase (AMPK)—the master metabolic switch of human cells.
Activation of AMPK promotes GLUT-4 glucose transporter translocation independent of insulin action. Our extraction methodologies utilize closed-loop ethanol/water isolation systems, guaranteeing that active anthraquinones and flavonoid markers maintain standard potency batch after batch.
Alpha-GPC (L-alpha-glycerylphosphorylcholine) crosses the blood-brain barrier rapidly to deliver bioavailable choline. Beyond cognitive benefit, it sparks growth hormone secretion and enhances peak twitch force in muscular exertion.
Because Alpha-GPC is highly hygroscopic, our automated capsule rooms maintain strict humidity controls below 30% RH, using specialized veggie HPMC shells to prevent shell softening and product degradation.
Eliminating supply chain vulnerability with centralized, certified contract manufacturing in Varna, Bulgaria
We empower growing brands to test innovative metabolic SKUs without trapping excess capital in warehouse stock. Ready-to-brand formulas launch with low risks and fast turnaround times.
High-speed encapsulation lines, high-shear powder mixers, automated pouch packaging, and gummy starch-less depositing lines guarantee seamless scaling as your retail distribution grows.
Every lot is manufactured within cleanroom environments adhering to strict European standards. Raw material validation, allergen controls, and batch testing prevent cross-contamination.
Navigating EFSA regulations (EC 1924/2006) and food information labeling rules (EU 1169/2011) is seamless. We supply verified Certificates of Analysis (COA), safety data sheets, and stability test reports.
As brand managers and contract buyers plan their product pipelines for 2025 and beyond, several structural shifts are influencing raw material selection, dosage formats, and marketing claims:
Essential guidance for brand founders, quality managers, and supply chain directors
For stock private-label formulations in standard capsule or powder formats, our MOQ starts at just 500 units per SKU. Custom formulations involving specialized botanical extracts, custom flavors, or unique gummy shapes generally require 3,000 to 5,000 units depending on raw material order limits.
Creatine can convert into inactive creatinine when exposed to high temperature and moisture over time. We utilize a low-heat, rapid-setting pectin formulation system alongside precise moisture control (< 0.6 aw). Every batch undergoes finished-product HPLC testing to confirm label claim potency.
Yes. Our in-house regulatory team reviews ingredient dosages against permitted EU novel food databases, validates nutrition and health claims against Regulation (EC) 1924/2006, and prepares label compliance files under Regulation (EU) 1169/2011.
Every commercial lot is released with a comprehensive Certificate of Analysis (COA). This documents active compound quantification (HPLC/UV), heavy metal screening (Lead, Cadmium, Mercury, Arsenic via ICP-MS), microbiological limits (TPC, Yeast & Mold, E. coli, Salmonella), and physical parameters (disintegration, density, moisture).
For existing catalog items with pre-approved label artwork, production and dispatch are completed within 3 to 4 weeks. Custom OEM projects, which involve raw material sourcing, flavor matching, pilot batching, and stability testing, typically require 6 to 8 weeks.
Our European manufacturing site operates strict Allergen Control Protocols under HACCP. Production schedules segregate allergen-containing raw materials (such as soy or dairy), and validated Cleaning-In-Place (CIP) procedures are verified with swab tests prior to line changeovers.
Whether you are expanding an established nutraceutical brand or introducing a disruptive GLP-1 support gummy, our formulation experts and production managers are ready to support your market growth.