Explore our certified, market-ready, and fully customizable dietary supplement formulations. Engineered for optimum bioavailability, physical stability, and international regulatory compliance.
The global wellness, active nutrition, and cognitive performance supplement industries are undergoing a fundamental structural transition. Driven by shifts in consumer preferences toward science-backed, highly targeted functional nutrition, brand owners and institutional distributors no longer seek standard contract packers. Instead, they require sophisticated technology partners. As a premier hub in international nutraceutical manufacturing, China has advanced from cost-efficient volume manufacturing to precision biochemical engineering, proprietary delivery matrices, and stringent international compliance alignment.
Modern buyers searching for the Top China White Label Manufacturers & Exporter look far beyond raw batch processing. Brand durability in highly regulated jurisdictions—such as the European Union (under EFSA regulations) and North America (governed by FDA 21 CFR Part 111)—demands full analytical transparency, raw material fingerprinting, batch-to-batch homogeneity, and validated shelf-life stability. OEM and ODM partnerships now center on how effectively a manufacturer can stabilize sensitive bioactive agents, such as micro-encapsulated creatine monohydrate, cholinergic compounds like Alpha-GPC, and plant-based protein isolates, while preventing organoleptic degradation.
Our proprietary dosage architecture engineered for complex active ingredient dispersion, preventing cross-degradation and maximizing intestinal kinetic absorption.
Fully automated cleanroom lines equipped with online NIR monitoring, heavy metal ICP-MS screening, and high-performance liquid chromatography (HPLC) testing.
Thermal-stable, pectin-based gummy extrusion technologies capable of loading high-dose ergogenic actives without sugar crystallization or moisture migration.
To achieve commercial success, private label supplements must solve real-world formulation bottlenecks. Commercializing complex functional formats—such as high-load ergogenic gummies, fast-dissolving low-carb electrolyte matrices, or standardized 10:1 botanical extracts—demands granular chemical control during manufacturing.
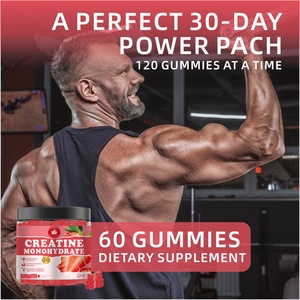
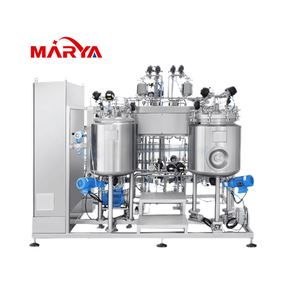
Creatine monohydrate is historically notoriously difficult to incorporate into functional confectionery formats due to its instability in aqueous solutions and tendency to convert into inactive creatinine under acidic processing temperatures. Utilizing the Marya Professional Formulation System, our facility deploys a micro-encapsulated hydrophobic matrix combined with low-temperature pectin cooking techniques. This ensures the creatine molecule remains stable, fully bioavailable, and non-degraded throughout its shelf life, offering fitness brands a market-leading alternative to traditional bulky powders.
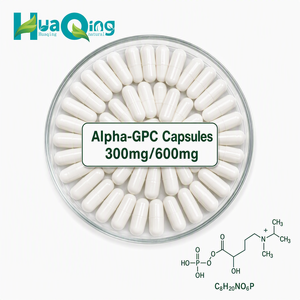
As cognitive health and executive performance supplements surge globally, Alpha-GPC has emerged as a cornerstone cholinergic active. However, raw Alpha-GPC is extremely hygroscopic, absorbing ambient moisture within minutes and destroying standard capsule integrity. Our white-label capsule manufacturing utilizes specialized vegetable HPMC shell technology and inert gas flushing during the encapsulation phase. Available in precise 300mg and 600mg dosages, our Alpha-GPC formulations remain free-flowing, stable, and compliant with EU and US dietary ingredient standardizations.
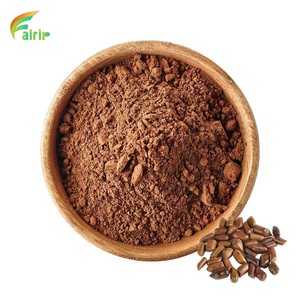
Phytochemical integrity defines high-grade botanical sourcing. Our 10:1 Cassia Seed Extract undergoes water-based, solvent-free counter-current extraction, followed by spray-drying to preserve delicate bio-actives including anthraquinones and glycosides. Every bulk batch comes accompanied by complete HPLC fingerprint analysis, heavy metal assays (Lead, Cadmium, Arsenic, Mercury under USP <2232> guidelines), and pesticide residue screenings, providing white-label clients with ironclad regulatory documentation for global export.
| Product Category | Active Core Dosage | Primary Delivery Technology | Quality & Compliance Standard | Target Health Benefit |
|---|---|---|---|---|
| Fitness Gummies | Creatine Monohydrate (Up to 1.5g/gummy) | Low-Temp Pectin Extrusion / Micro-encapsulated | cGMP, Non-GMO, Sugar-Free Options | Cellular Hydration & Skeletal Muscle Growth |
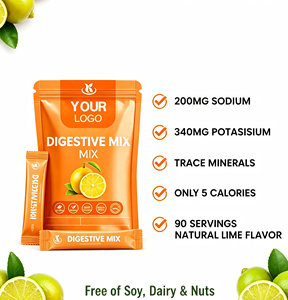
| Electrolyte Powders | Sodium, Potassium, Magnesium, Zinc Stack | Agglomerated Instantized Blend (Low-Carb) | HACCP, ISO22000, Zero Artificial Fillers | Rapid Intracellular Rehydration & Cardiac Health |
| Nootropic Capsules | Alpha-GPC 300mg / 600mg (Purity >99%) | HPMC Veggie Capsule / Moisture-Lock Barrier | Third-Party HPLC Verified, Allergen-Free | Acetylcholine Synthesis & Executive Focus |
| Botanical Powders | Cassia Seed Extract (10:1 Ratio) | Solvent-Free Counter-Current Extraction | Food-Grade, Heavy Metal & Pesticide Screened | Metabolic Balance & Digestive Wellness |
| Plant Proteins | Pea & Brown Rice Isolate Blend (>80% Protein) | Enzymatic De-bittering & Micronization | Vegan, Complete Amino Acid Profile, Kosher/Halal | Lean Muscle Protein Synthesis & Recovery |
To remain competitive in an increasingly crowded retail and direct-to-consumer (D2C) marketplace, procurement managers must anticipate systemic shifts in supply chain dynamics, sustainability mandates, and consumer delivery expectations.
Consumer pill fatigue is driving rapid market migration toward functional gummies, effervescent powders, and liquid sachets. Contract manufacturers must possess advanced flavor-masking capabilities to neutralize bitter botanicals and metallic mineral salts without inflating caloric content.
Regulators and modern consumers demand complete traceability from farm to finished package. Leading Chinese exporters now offer full batch documentation, including genomic plant identification, origin sourcing certificates, and carbon-neutral processing logs.
The era of requiring multi-ton opening orders is fading. Successful exporters support fast-growing brands with flexible, low-MOQ pilot runs (starting as low as 500-1,000 units for stock formulas), allowing rapid real-world A/B testing before mass scale-up.
Operating out of state-of-the-art pharmaceutical-grade cleanrooms, our facility represents the pinnacle of Chinese contract manufacturing. We seamlessly bridge the gap between low-cost manufacturing scale and high-stringency Western regulatory expectations.
From raw material procurement and custom flavor development to custom bottle blowing, graphic design, and export customs clearance—we handle every link of your supply chain under one roof.
Our regulatory affairs team provides complete Certificates of Analysis (CoA), Stability Test Reports, TSE/BSE-free attestations, and compliant label content verified against local food safety laws.
Computer-controlled automated batching systems eliminate human error, ensuring that your protein powders dissolve identically and your gummies maintain uniform texture with every single shipment.
Essential guidance for brand founders, product managers, and global procurement leads considering Chinese OEM/ODM partnerships.
MOQs depend on the delivery format. For standard stock capsule formulations, opening MOQs start as low as 500 to 1,000 bottles per SKU. For custom-flavored powders, functional gummies, or complex plant protein formulations requiring custom film printing, baseline MOQs typically range from 3,000 to 5,000 units to optimize production economics and raw material setup costs.
Our manufacturing plant operates strictly under cGMP (21 CFR Part 111) and ISO22000 standards. Every batch undergoes mandatory raw material identification testing, in-process blend uniformity checks, and finished product assay testing by independent accredited third-party laboratories. We supply comprehensive analytical dossiers required by customs and food safety authorities worldwide.
Yes. Our in-house flavor chemistry laboratory specializes in developing custom natural flavor matrices (including berry, citrus, tropical, and mint profiles) and sugar-free sweetener stacks (utilizing monk fruit, stevia, or erythritol). We provide benchtop R&D samples for organoleptic evaluation prior to commercial batch execution.
For established formulations with approved label artwork, typical lead times are 3 to 4 weeks for manufacturing, quality testing, and packaging release. Novel custom formulations requiring stability benchmarking or specialized raw material sourcing may require 5 to 6 weeks. Express air freight and ocean freight shipping options are supported.
All incoming active pharmaceutical ingredients (APIs), botanical extracts, and excipients are quarantined upon arrival. They undergo rigorous chemical verification via FTIR spectrometry, HPLC purity screening, and microbiological assays (E. coli, Salmonella, yeast, and mold count) before release into production cleanrooms.
Consult with our senior formulation engineers and export specialists today. Get a tailored quotation, request benchtop samples, or review technical specifications for your next product launch.