Explore our high-demand OEM/ODM product portfolio engineered for global market compliance, optimal bioavailability, and turnkey commercialization.
The global sports nutrition and functional food industry is undergoing a structural transformation driven by heightened consumer demand for clean-label, bioavailable, and targeted macromolecular nutrition. As the global epicenter for raw material processing, enzyme engineering, and automated high-throughput packaging, China stands at the forefront of protein powder contract manufacturing (OEM/ODM). Modern B2B procurement demands far more than basic powder blending; global brands require pharmaceutical-level quality systems, micro-encapsulation technologies, granular solubility optimization, and rigorous heavy metal remediation.
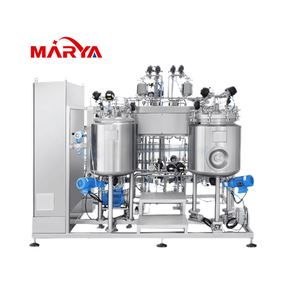
As a leading Chinese protein powder manufacturer, our production ecosystem leverages state-of-the-art processing infrastructure—such as the Marya Automated Formulation System—to deliver custom whey isolates, plant-based protein blends, and functional protein-peptide complexes. By integrating raw material synthesis directly with Class 100,000 cleanroom packaging, we eliminate supply chain friction, lower unit procurement costs, and guarantee strict compliance with international regulatory frameworks including FDA 21 CFR Part 111, EU Food Safety Standards, and ISO 22000 certification.
Information Gain Insight: The modern protein buyer is pivoting away from standard concentrate blends toward functionalized protein isolate matrices enriched with ergogenic aids (e.g., Creatine Monohydrate, Alpha-GPC) and rapid-osmolality electrolyte transport systems. Contract manufacturing must ensure thermal stability during spray drying to preserve protein native structures and prevent amino acid denaturation.
Our manufacturing complex supports a complete spectrum of dairy and plant-derived protein substrates, each subjected to advanced physical treatment to guarantee particle size uniformity, instant dispersibility, and superior sensory profiles:
• Cross-Flow Microfiltration (CFM) Whey Isolates: Utilizing low-temperature membrane filtration, our whey protein isolates retain key bioactive immunoglobulins and lactoferrin fractions while achieving >90% dry-basis protein content with virtually zero lactose or fat.
• Synergistic Plant-Based Iso-Proteins: Combining yellow pea protein isolate (85%), organic brown rice protein, and pumpkin seed peptide fraction allows us to engineer complete amino acid profiles that achieve a PDCAAS (Protein Digestibility-Corrected Amino Acid Score) of 1.0, overcoming traditional plant protein taste and solubility drawbacks through ultrasonic organoleptic refining.
• Enzymatic Hydrolysates: Bio-engineered peptide fragments optimized for rapid gastric emptying and direct cellular uptake, ideal for post-workout recovery, clinical nutrition, and sensitive digestion formulations.
Building world-class sports nutrition products requires multi-disciplinary engineering, strict regulatory backing, and scalable supply chain operations.
Operating under Class 100,000 cleanroom environments with continuous climate, humidity, and airborne particulate monitoring to completely prevent cross-contamination across allergen lines.
Utilizing high-precision gravimetric micro-dosing automation to guarantee batch-to-batch content uniformity for micro-ingredients such as Alpha-GPC, vitamins, and specialized botanicals.
Every raw material and finished batch undergoes rigorous testing via HPLC, GC-MS, and ICP-MS for active assay assaying, micro-biology clearance, and heavy metal limits (Pb, Cd, Hg, As).
Full support for EU Novel Food verification, US FDA GRAS dossiers, Halal, Kosher, and zero-banned-substance WADA testing documentation for athletic performance lines.
Turnkey packaging choices ranging from 100% recyclable HDPE tubs, laminated aluminum barrier doypacks, to single-serve stick-packs with nitrogen flushing for extended shelf life.
Proprietary flavor masking technology that eliminates the bitter, earthy off-notes of botanical extracts, BCAAs, and plant proteins using natural flavor systems and stevia/monk fruit blends.
The sports nutrition dynamic has evolved beyond simple macronutrient replenishment into holistic physical and cognitive optimization. As brands navigate an increasingly competitive market, successful product positioning requires leveraging key macro-trends in formulation design:
Single-benefit protein powders are increasingly viewed as legacy products. Next-generation consumer demand favors integrated "all-in-one" matrixes. Formulations that blend high-purity protein isolate with cognitive enhancers like Alpha-GPC or L-Theanine, alongside rapid-hydrating electrolyte minerals (Potassium Citrate, Magnesium Glycinate), capture higher retail price points and deliver measurable performance benefits. Our factory specializes in dry-blending delicate thermolabile active compounds into uniform protein powders without phase separation.
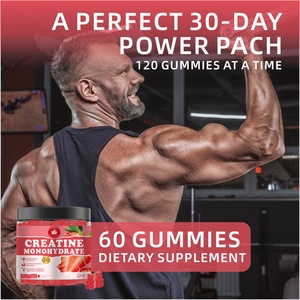
While traditional protein tubs remain core market drivers, active lifestyle consumers increasingly demand convenient, on-the-go delivery formats. The development of heat-stable Creatine Monohydrate Gummies and Protein-infused Gummy Confections represents one of the fastest-growing OEM product segments. By utilizing pectin-based hot-fill processes that avoid degrading active amino structures, our facility manufactures functional gummies with precise active dosing per serving.
Consumer transparency demands zero artificial colors, synthetic flavors, or obscure chemical anti-caking agents. Modern procurement focuses on precision-fermented amino acids, non-GMO botanical extract fillers (such as Cassia Seed or soluble acacia fiber), and natural flavor carrier systems. Furthermore, complete allergen isolation (Gluten-Free, Dairy-Free, Soy-Free) is mandatory for top-tier international retail placement.
Procuring bulk sports nutrition supplements from China requires a sophisticated supply chain roadmap focused on quality assurance, lead-time stabilization, and total cost of ownership (TCO) optimization. Brands must evaluate prospective contract manufacturers against four critical technical vectors:
Supply Chain Security Advisory: Volatility in global raw whey prices and ocean freight schedules highlights the importance of working with manufacturers that maintain strategic buffer stocks of premium milk protein isolate, pea protein, and key functional actives (Creatine, Electrolyte salts).
1. Analytical Verification & Traceability: Reliable suppliers must furnish batch-specific Certificates of Analysis (COA) from ISO 17025 accredited third-party laboratories detailing protein assay levels, nitrogen factors, heavy metal screening, and microbial verification.
2. Particle Dynamics & Instantization Technology: Powder solubility is directly governed by mesh size and agglomeration technology. Our spray-drying and lecithin-instantization processes yield 80–200 mesh powders that dissolve effortlessly in cold liquids without clumping or foam retention.
3. Minimum Order Quantity (MOQ) Scalability: Emerging brands require flexible low-MOQ starting tiers (e.g., 500–1,000 units for stock formulations) to validate market traction, with seamless scaling pathways to 50,000+ unit runs as demand grows.
Essential guidance for brand owners, product managers, and supply chain directors sourcing protein supplements from China.
For stock private label formulas with standard flavor profiles, our MOQ starts as low as 500 to 1,000 tubs. For full custom formulations requiring specific flavor development, unique active ingredients, or customized printed packaging bags/tubs, MOQ typically ranges from 2,000 to 3,000 units per SKU.
We perform rigorous HPLC and total nitrogen (Kjeldahl/Dumas method) testing on both raw protein inputs and finished product batches. We explicitly guarantee zero added free-form amino acid padding (spiking); our lab certificates confirm true protein fractions from intact isolate or hydrolysate sources.
Yes. Our regulatory compliance team reviews every ingredient dosage against EU Novel Food guidelines, EFSA health claim regulations, and US FDA GRAS lists. We prepare fully compliant label layout files, including accurate Nutritional Facts panels and allergen statements for your target destination.
We provide a comprehensive array of packaging solutions including recyclable HDPE/PET plastic jars (1lb, 2lb, 5lb sizes), matte/gloss laminated aluminum barrier doypacks, and single-serve stick packs. All packaging options feature induction sealing and optional nitrogen flushing for optimal shelf-life stability.
Once flavor sampling is approved and label artwork is finalized, standard manufacturing lead time is 3 to 4 weeks. Sourcing specialized custom raw materials or printed packaging films may add 1 to 2 weeks. Expedited production runs are available for established repeat partners.
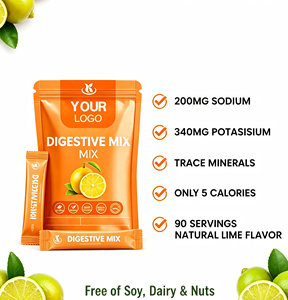
Yes, we specialize in advanced delivery formats including Creatine Monohydrate Gummies, Electrolyte Hydration Drink Mixes, Alpha-GPC Nootropic Capsules, and Botanical Extract Powders. All products run through dedicated specialized cleanroom lines.