Production Portfolio
High-Purity Standardized Raw Ingredients & Formulations
Direct supply from our certified European-standard manufacturing facility. Fully documented with HPLC, GC-MS, and microbiological Certificates of Analysis (CoA).
VLAND High Quality Food Grade Aminopeptidase Enzyme For Protein Hydrolyzate
Get a Quote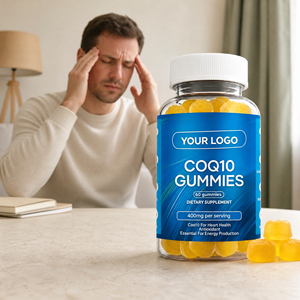
Mango Flavor Food Grade Concentrated Easy Chew CoQ10 Gummies
Get a Quote
Premium Vegan Bio Moringa Powder Bulk Packaged Herbal Supplements
Get a Quote
3-FL HMOs 99% HPLC Precision Fermentation No Endotoxin Powder
Get a Quote
High Purity 30000U/ml Neutral Proteolytic Enzyme Protease Food Additive
Get a Quote
White Kidney Bean Extract Powder Phaseolin 2% MOQ 1kg CAS: 37831-70-2
Get a Quote
Raw Crystal Pure Dimethyl Terephthalate Powder CAS 120-61-6 DMT Bulk
Get a Quote
1,000,000+
Daily Capsule Unit Capacity
99.0%
HPLC Assay Purity Standard
< 0.005 EU/mg
Ultra-Low Endotoxin Limit
30+
Global Export Markets
Enterprise & Facility Infrastructure
cGMP European Manufacturing Operations & Technical Mastery
Engineered to eliminate supply chain volatility through precision biological manufacturing and rigorous quality control.
Integrated European Quality Management & Operational Scalability
In the global B2B nutraceutical supply chain, brand scalability hinges on absolute manufacturing consistency and flawless regulatory documentation. Operating from our advanced facility in Varna, Bulgaria, our operations provide full end-to-end integration for dietary supplement brands, pharmaceutical distributors, and functional food innovators. By unifying raw material synthesis, bioprocess extraction, galenic formulation, and primary packaging under a single certified roof, we guarantee batch-to-batch reproducibility that meets the stringent demands of European and global regulatory bodies.
Our facility operates strictly within GMP (Good Manufacturing Practice), HACCP (Hazard Analysis Critical Control Point), and ISO 22000 quality management systems. Every production lot undergoes rigorous multi-stage validation, including raw material identification, mass spectrometry, heavy metal quantification via ICP-MS, and microbiological screening. This technical infrastructure protects brand equity and ensures uninterrupted market entry across the EU, UK, North America, and the Middle East.
Core Technical Capabilities & Contract Manufacturing Scope
- Precision Fermentation & Enzymatic Hydrolysis: Specialized strain selection and bioreactor scaling yielding high-purity bioactive molecules such as 3'-Fucosyllactose (3-FL HMOs) with purity exceeding 99.0% by HPLC.
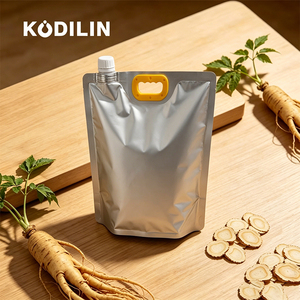
- Plant Cell Culture Biotechnology: Sustainable, eco-friendly bioreactor propagation of adventitious roots (e.g., KODILIN Ginseng), eliminating heavy metal contamination, pesticide residues, and seasonal yield fluctuations inherent to traditional agriculture.
- Solid & Liquid Dosage Galenics: High-speed encapsulation of two-piece hard gelatin and HPMC vegan capsules, tablet compression, micro-encapsulated functional powders, single-serve liquid sachets, and precision pectin/gelatin chewables.
- Allergen-Controlled High-Volume Lines: Dedicated production zones with automated clean-in-place (CIP) protocols to handle plant proteins, marine collagen peptides, and botanical extracts without cross-contamination.
Regulatory Compliance & EU dossiers
Full assistance with Regulation (EU) 1169/2011 labeling laws, Regulation (EC) 1924/2006 health claim verifications, and Novel Food status filings to ensure friction-free cross-border trade.
Custom OEM/ODM Formulation Matrix
In-house laboratory R&D to tailor dosage architectures, flavor profiles, particle size distribution, and dissolution kinetics aligned with target price points and clinical efficacy.
Flexible Low-MOQ Entry to Full Scale
Support for emerging brands starting from 500 units on stock SKUs, seamlessly scaling to continuous multi-ton container shipments for global distribution enterprise clients.
Market Intelligence
Strategic Procurement Trends in Bio-Nutraceuticals (2025–2030)
Analysis of shift drivers altering global bulk raw material sourcing, synthetic biology, and regulatory scrutiny.
1. Transition to Precision Fermentation & Human Milk Oligosaccharides
The global market for pediatric and adult gut health is rapidly pivoting away from crude prebiotic fibers toward ultra-pure, bio-identical sugars derived via precision fermentation. Ingredients like 3'-Fucosyllactose (3-FL HMOs) represent the peak of this evolution. Procurement teams are prioritizing suppliers capable of demonstrating ultra-low endotoxin levels (<0.005 EU/mg) and non-GMO recombinant host processing. Precision fermentation delivers unprecedented purity, complete decoupling from agricultural climate risks, and verified bio-equivalence to natural human bio-fluids.
2. Botanical Extraction via Plant Cell Culture Bioreactors
Wild harvesting and traditional soil cultivation of medicinal roots (such as Panax Ginseng) face increasing severe heavy metal accumulation, wild stock depletion, and batch potency variability. Advanced procurement strategies now mandate adventitious root cell culture techniques. By cultivating plant biomass in sterile liquid bioreactors, biomanufacturers yield consistent bioactive ginsenoside profiles (e.g., 10% active liquid titrations) free from microplastics, polycyclic aromatic hydrocarbons (PAHs), and synthetic pesticides.
3. Targeted Biocatalysis & Targeted Enzyme Hydrolysis
In functional food processing and protein modification, crude proteases are being systematically replaced by specialized exopeptidases and endopeptidases. Industrial buyers utilize enzymes like high-purity Aminopeptidase to cleave N-terminal amino acids specifically, eliminating bitter peptides in plant and whey protein hydrolysates. This precise enzymatic tuning enhances solubility, speeds gastrointestinal absorption, and yields clean-tasting functional protein beverages without added artificial flavor masking agents.
4. Phaseolin-Induced Amylase Inhibition for Metabolic Health
With metabolic health and weight management dominating consumer intent, the demand for natural alpha-amylase inhibitors has surged. Standardized extract powders derived from Phaseolus vulgaris, specifically Phaseolin 2% titrations, are rapidly becoming core actives in carbohydrate-blocking formulations. Enterprise buyers require verified biological activity unit assays alongside traditional chemical identification to guarantee physiological efficacy in finished dosage forms.
Global Industry Growth Drivers & Category Evolution
The global nutraceutical market is transitioning from generic multivitamin blends toward clinically validated, mechanism-driven active ingredients. Brand owners and private label distributors must adapt to three structural macro trends driving consumer purchasing behavior and retail distribution requirements:
A. The Convergence of Food Grade Delivery & High-Dosing Efficacy
Consumer pill fatigue has permanently altered format preferences. Modern consumers demand active pharmaceutical-grade molecules delivered in consumer-friendly formats such as chewable pectin gummies, effervescent powders, and liquid concentrates. Manufacturing concentrated active ingredients—such as Coenzyme Q10 (CoQ10) inside stable pectin gummy matrices—requires specialized temperature control and emulsification engineering to prevent nutrient thermal degradation during mass extrusion. Factories capable of maintaining active potency within pleasant galenic deliveries are capturing market share twice as fast as traditional tablet presses.
B. Sustainable Clean-Label Traceability & Vegan Compliance
Regulatory bodies and consumers alike are scrutinizing full supply chain transparency. Ingredients like organic, non-GMO bio moringa powder must possess complete analytical traceability from origin soil testing to final drum milling. Clean-label standards mandate zero synthetic excipients, silicon dioxide replacement with natural rice hulls, and 100% plant-derived encapsulation. Exporters holding verified organic and vegan certifications enjoy preferential shelf placement and premium retail price positioning across Tier-1 markets.
C. High-Purity Industrial Additives & Specialized Chemical Excipients
Beyond consumer dietary supplements, the crossover between specialized organic chemical synthesis and food-grade excipient processing has narrowed. Pure crystalline compounds such as Dimethyl Terephthalate (DMT, CAS 120-61-6) serve as critical precursors in polymer synthesis, barrier packaging films, and specialized industrial applications. Exporters possessing rigorous chemical quality control, consistent particle mesh sizing, and secure international hazard-handling shipping frameworks provide vital stability to global manufacturing supply chains.
Technical Insights
Frequently Asked Questions for Industrial Procurement & OEM Partners
Addressing core technical, regulatory, and logistics queries for international brand managers and purchasing directors.
What analytical testing methods are utilized to verify batch purity and bioactive concentration?
Every production batch undergoes full analytical profiling before release. We utilize High-Performance Liquid Chromatography (HPLC) for quantification of active marker compounds (e.g., Phaseolin titrations, Ginsenosides, 3-FL HMOs). Gas Chromatography-Mass Spectrometry (GC-MS) is employed for volatile organic compound screening, and Inductively Coupled Plasma Mass Spectrometry (ICP-MS) verifies that heavy metals (Lead, Cadmium, Mercury, Arsenic) remain well below EU and USP safety thresholds. A comprehensive Certificate of Analysis (CoA) is attached to every dispatch.
How does precision fermentation for 3-FL HMOs achieve zero-endotoxin parameters for infant formula?
Our 3-FL HMO synthesis utilizes genetically stable, non-pathogenic expression strains cultivated under strict bio-reaction conditions. Post-fermentation recovery involves multi-stage ultrafiltration, ion-exchange chromatography, and crystallization steps specifically validated to eliminate lipopolysaccharides (LPS). Final endotoxin testing via Limulus Amebocyte Lysate (LAL) assay confirms levels below 0.005 EU/mg, meeting global safety standards for sensitive infant nutrition and medical food formulations.
What are the lead times for custom OEM formulation development vs. bulk ingredient dispatch?
Standard catalog raw ingredients (in stock) ship within 3 to 5 business days following order confirmation and export documentation approval. Custom contract manufacturing projects—including custom flavor development, tablet tooling, encapsulation, and customized secondary packaging—typically require 3 to 5 weeks from final sample sign-off and packaging artwork clearance.
Can you assist with European Union food safety compliance and label claim verification?
Yes. Our in-house regulatory affairs department systematically reviews product formulations against EU Novel Food regulations, local permitted substance lists, and Regulation (EC) 1924/2006. We assist in structuring compliant nutrition panels, ingredient declarations under Regulation (EU) 1169/2011, and allergen statements to eliminate customs holds and regulatory rejection upon import into European ports.
What parameters govern the bio-activity and enzymatic strength of your custom proteases?
Our enzyme products, such as Neutral Proteolytic Enzyme Protease (30,000 U/ml) and Aminopeptidases, are assayed for enzymatic activity units per gram/milliliter under standardized temperature (°C) and pH conditions. We provide exact activity profile curves, optimal processing parameters, and thermal inactivation guidance to allow food technicians to integrate the enzymes smoothly into protein hydrolysis or brewing lines.
What are the minimum order quantities (MOQ) for custom contract manufacturing projects?
We maintain accessible entry parameters to support scaling enterprises. Selected stock encapsulation and bottling projects start from 500 units per SKU. Bulk extract powders and custom enzyme blends typically start at 1 kg to 25 kg fiber drum quantities depending on raw material synthesis economics and specialized packaging requirements.
Partner with a Certified European OEM Manufacturer
Consult with our technical sales engineers, request raw material samples, or obtain custom formulation quotations tailored to your exact regulatory target market.
Get a Quote