Directly engineered in our state-of-the-art Marya cleanroom facility, featuring flexible MOQ options, strict dosage uniformity, and full EU/FDA compliance.
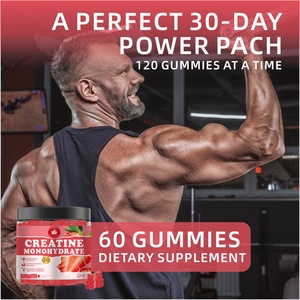
Supports cellular hydration, explosive power, and skeletal muscle growth. Available for private label OEM with tailored flavor profiles.
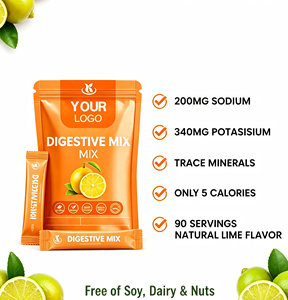
Heart-healthy, low-carb hydration blend formulated for adult cellular balance. GMP-certified OEM contract blending.
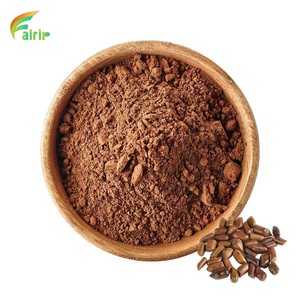
High-purity food grade 10:1 standardized extract powder. Ideal for bulk capsule encapsulation and digestive health formulas.
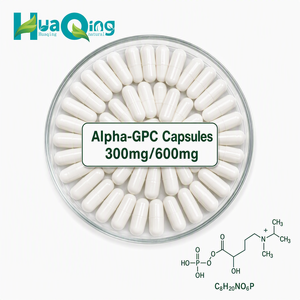
Premium bioavailable choline supplement for cognitive enhancement and focus. HPMC vegetarian shell encapsulation.
Custom vegan amino acid complex formulated with clean-label botanical proteins. Bulk powder supply and private labeling.
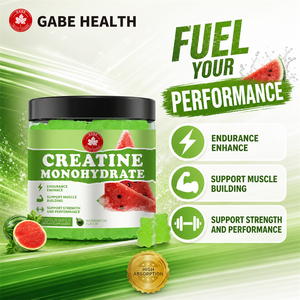
Non-GMO athletic recovery gummies engineered for optimal muscle absorption. Custom ODM/OEM matrix development.
Ultra-micronized sports nutrition powder engineered for rapid dissolution and maximum stability. Direct factory wholesale.
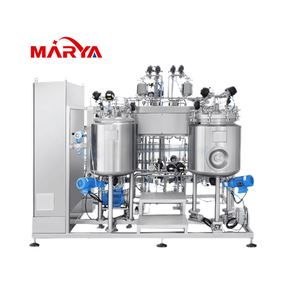
Advanced HVAC & cleanroom pharmaceutical systems providing zero cross-contamination capsule manufacturing.
Integrating pharmaceutical precision with agile contract manufacturing to power scalable growth.
Our facility is equipped with Marya Class D automated HVAC cleanroom environments, controlling humidity, particulate density, and air pressure to prevent active ingredient degradation during encapsulation.
Every capsule batch undergoes stringent in-process weight checks, disintegration testing, and microbiological evaluation under fully documented ISO 22000 and Good Manufacturing Practice compliance.
From size #00 to #4 hard gelatin, vegetarian HPMC, enteric-coated capsules, to liquid-filled softgels—our R&D laboratory optimizes fill mass density, dissolution rate, and thermal stability.
The global dietary supplement market is experiencing a profound paradigm shift. As consumers demand clean-label formulations, higher bioavailability, and transparent raw material sourcing, brand owners must partner with advanced contract manufacturers capable of executing precise capsule technology. As a premier **China bulk capsules exporter and contract manufacturer**, our production operations combine automated pharmaceutical cleanroom systems with high-speed encapsulation machinery to deliver uncompromised quality to international brand owners, distributors, and pharmaceutical entities across Europe, North America, the Middle East, and Asia-Pacific.
SEO & Procurement Key Takeaway: Modern capsule procurement is no longer just about per-unit cost. Leading brands prioritize dosage accuracy, low moisture degradation, non-GMO shell chemistry (HPMC/Pullulan), cleanroom environmental controls, and comprehensive COAs validating heavy metal, pesticide, and microbiological safety.
Encapsulation is a complex mechanical and chemical engineering process. Achieving weight uniformity within strict tolerance bands (under ±1.5% variance) requires rigorous control of powder flowability, bulk density, particle size distribution (mesh size), and ambient moisture control within the manufacturing suite.
Choosing the correct raw shell material is critical for shelf-life stability, target market compliance (Halal, Kosher, Vegan), and active ingredient compatibility:
| Shell Material Type | Source Origin | Moisture Content | Key Advantages | Best Formulations |
|---|---|---|---|---|
| Bovine Gelatin | Pharmaceutical Grade Collagen | 13.0% – 16.0% | Cost-effective, robust oxygen barrier, rapid stomach dissolution | Standard vitamins, minerals, non-hygroscopic herbal powders |
| HPMC (Vegetarian) | Plant Cellulose (Pine / Wood Fiber) | 4.5% – 7.0% | Non-GMO, Vegan, Halal/Kosher certified, resistant to cross-linking | Hygroscopic botanicals, moisture-sensitive probiotics, Alpha-GPC |
| Pullulan | Fungal Fermentation (Tapioca starch base) | 10.0% – 14.0% | Ultra-high oxygen barrier, 100% natural organic claims | Oxidation-sensitive antioxidants, premium anti-aging complexes |
| Enteric HPMC | Acid-Resistant Cellulose Polymers | 5.0% – 8.0% | Passes through stomach acid (pH 1.2), dissolves in intestine (pH 6.8) | Probiotics, enzyme blends, targeted intestine delivery formulas |
Raw botanical powders and crystalline active ingredients—such as Creatine Monohydrate 200 Mesh or high-potency Alpha-GPC powder—present unique handling challenges. Hygroscopic materials absorb atmospheric moisture, leading to clumping, sticky dosing discs, and weight variation during high-speed encapsulation.
Our facility utilizes specialized 3D dry-powder blending technology combined with vacuum conveyancing under controlled humidity conditions (relative humidity maintained below 35%). When necessary, specialized non-GMO excipients such as rice hull extract or pharmaceutical-grade silica are engineered into the matrix to ensure uniform tamping pin insertion and precise capsule fill volumes.
Procurement executives facing volatile global logistics costs and shifting regulatory landscapes must adapt to several emerging trends governing the international contract manufacturing ecosystem:
While hard gelatin and HPMC capsules remain the gold standard for high-potency, bitter-tasting, or oxygen-sensitive active ingredients, consumer preference for novel delivery forms—such as functional gummies and effervescent powders—is surging. Brands that maintain a dual supply portfolio consisting of **bulk capsules** for clinical-potency SKUs and **creatine/electrolyte gummies** for lifestyle nutrition achieve higher customer retention and brand equity.
Regulatory authorities including the European Food Safety Authority (EFSA) and the U.S. FDA have heightened scrutiny regarding synthetic additives, titanium dioxide colorants (E171), and ethylene oxide (EtO) residues. Modern importers require contract manufacturers to supply full chromatographic fingerprinting (HPLC, GC-MS) and heavy metal detection via Inductively Coupled Plasma Mass Spectrometry (ICP-MS) down to parts-per-billion (ppb) sensitivity.
Information Gain Insight: Our manufacturing plant enforces 100% Titanium-Dioxide-Free capsule production. We utilize natural colorants derived from chlorophyll, purple carrot, and spirulina extracts, allowing global distributors to meet strict EU consumer safety mandates effortlessly.
Traditional contract manufacturing often demanded massive initial capital commitment with minimum order quantities exceeding 50,000 to 100,000 bottles. Recognizing the market demand for agile brand expansion, our strategic operational framework offers **flexible entry MOQs starting at 500 bottles per SKU** for select stock formulations, while seamlessly scaling to multi-million unit mass production runs for established retail buyers.
Creatine Monohydrate remains one of the most clinically validated sports nutrition ingredients globally. However, delivering stable, palatable, non-gritty creatine requires expert processing. Our ultra-micronized 200-mesh bulk creatine powder ensures rapid liquid suspension without sedimentation. Furthermore, our **Creatine Fitness Gummies** utilize pectin-based matrix technology that resists heat melting up to 45°C, ensuring international freight integrity.
Alpha-Glycerophosphocholine (Alpha-GPC) is highly deliquescent—meaning it rapidly liquefies upon exposure to ambient air. Encapsulating 300mg to 600mg dosages of Alpha-GPC requires specialized climate-controlled encapsulation suites. By pairing high-purity Alpha-GPC with Low-Moisture HPMC shells, we ensure zero capsule deformation, zero sticky residues, and long-term shelf stability.
Botanical extracts such as Cassia Seed 10:1 extract require precise batch-to-batch standardization of bioactive markers. Raw botanicals undergo aqueous-alcohol extraction, spray-drying, and heavy metal remediation. The resulting fine powder is encapsulated or supplied in bulk containers with complete Certificate of Analysis (COA) documentation for international custom release.
Central to our enterprise manufacturing superiority is the deployment of the **Marya Cleanroom HVAC and Automated System**. Dietary supplement safety begins with environmental control:
| Quality Assurance Checkpoint | Testing Methodology | Compliance Standard | Impact on Bulk Buyer |
|---|---|---|---|
| Disintegration Time | USP <701> Disintegration Tester | < 15 Minutes (Gelatin/HPMC) | Guarantees active ingredient bioavailability |
| Heavy Metal Residue | ICP-MS (Pb, Cd, Hg, As) | Strict EU Reg (EC) No 1881/2006 | Prevents border rejections and customs holds |
| Microbiological Count | Automated Plate Count & PCR | TPC < 1,000 CFU/g; Zero Pathogens | Protects brand reputation & end-user safety |
| Fill Mass Uniformity | Analytical 4-Decimal Balance Check | Within ±1.5% Target Weight | Ensures accurate label claim dosage per capsule |
Essential guidance on lead times, certifications, regulatory compliance, and custom formulation workflows.
For stock formulas in standard bottle sizes, our MOQ starts at just 500 units. For custom formulations requiring specialized raw material sourcing or custom-printed capsule shells, MOQs generally start at 100,000 loose capsules or 1,000 finished retail bottles.
Our manufacturing facility operates strictly under Good Manufacturing Practice (GMP), ISO 22000 Food Safety Management, and HACCP standards. Products exported to specific regions can also be accompanied by Halal, Kosher, and Certificate of Free Sale (CFS) documentation.
We utilize the Marya Cleanroom HVAC system with positive pressure differential controls and HEPA filtration. Equipment undergoes validated multi-step sanitization protocols between batches, verified by environmental swab testing prior to line clearance.
Yes. We offer capsule sizes ranging from #000, #00, #0, #1 to #4. Shell options include transparent, opaque, single-color, or dual-color combinations. We also offer axial or radial brand logo printing using non-toxic food-grade inks.
For standard stock formulas, manufacturing and packaging take approximately 2 to 3 weeks. Custom formulations requiring raw material synthesis, pilot batch stability testing, or custom printed packaging typically take 4 to 6 weeks.
Yes. Our dedicated regulatory affairs team verifies raw material dosages against EU Novel Food regulations, check claims against Regulation (EC) 1924/2006, and provides full Master Batch Records, COAs, and stability documentation required for international registration.
Partner with a certified contract manufacturer engineered for precision, regulatory compliance, and global growth. Contact our technical team today to discuss custom formulations, raw material specs, or bulk wholesale quotes.