Engineered for maximal strain viability, gastrointestinal survival, and targeted wellness outcomes. Available for private label customization.
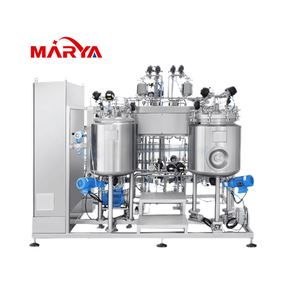
The global demand for human microbiome solutions has fundamentally shifted the paradigm for commercial probiotic manufacturing. China’s advanced biotech infrastructure now leads the world in high-density submerged fermentation technology, achieving cell concentrations exceeding 500 Billion CFU/g prior to freeze-drying. Historically, probiotic powders suffered severe viability decay during processing, storage, and gastric passage. Modern tier-1 Chinese factories have effectively solved these stability bottlenecks through bio-engineering innovations.
By implementing multi-layer microencapsulation (including sodium alginate, lipid coatings, and prebiotic matrices), high-grade probiotic powders manufactured in China demonstrate superior gastrointestinal resilience. Strain survival rates under simulated gastric fluid conditions (pH 1.5–2.0 for 2 hours) now consistently exceed 92%, ensuring that targeted live microorganisms reach the lower intestine intact. Furthermore, industrial-scale lyophilization protocols utilize specialized cryoprotectants (trehalose, skim milk solids, and protective amino acids) to preserve cell membrane integrity during cryogenic freezing.
In probiotic manufacturing, metabolic latency is paramount. Water activity ($a_w$), rather than total moisture content, directly dictates strain degradation over shelf life. Premier Chinese contract manufacturing plants operate fully enclosed, humidity-controlled HVAC systems maintaining relative humidity (RH) below 30% and ambient temperatures under 20°C throughout blending and packaging.
By maintaining finished powder water activity at $a_w \le 0.15$, bacterial metabolic activity is completely arrested. This technological rigor allows top-tier factories to guarantee target CFU counts at the end of a 24-month room-temperature shelf life, eliminating the mandatory refrigerated supply chain constraints that previously burdened international distributors.
Our state-of-the-art facility combines pharmaceutical-grade engineering with scalable commercial manufacturing to yield uncompromised product purity.
Operating inside ISO Class 7 (Class 100,000) cleanrooms equipped with positive pressure, HEPA filtration, and automated CIP/SIP sanitation loops to guarantee zero cross-contamination.
Expert bio-engineers tailor multi-strain probiotic matrices, combining *Lactobacillus*, *Bifidobacterium*, and spore-forming *Bacillus* strains with synergistic prebiotics and digestive enzymes.
Every batch undergoes 16S rRNA gene sequencing for absolute strain verification, flow cytometry for live/dead cell ratio verification, and heavy metal/microbial pathogen screening.
Fully compliant with US FDA NDI/GRAS guidelines, EU EFSA Novel Food regulations, TGA standards, and certified under cGMP, HACCP, ISO22000, FSSC22000, Halal, and Kosher.
Flexible manufacturing capacity accommodates pilot testing from 500 units up to high-capacity bulk production exceeding 50 million sachets and jars per month.
Automated sachet and jar filling lines utilize multi-layer aluminum foil barrier packaging with continuous nitrogen flushing ($O_2 < 1.0\%$) to minimize strain oxidation.
Key analytical insights for brand owners, supply chain directors, and product developers seeking competitive differentiation.
While live bacterial cultures dominate the current market, procurement data indicates rapid growth in inactivated microbial cells (Postbiotics) and cell-free supernatants containing functional metabolites (short-chain fatty acids, bacteriocins, and exopolysaccharides). Postbiotics offer complete formulation stability in beverage, gummy, and baked food matrices where moisture and processing heat traditionally kill live probiotics. Leading Chinese factories are expanding thermal inactivation lines to supply high-purity postbiotic powders for functional food integration.
Spore-forming probiotics have surged in B2B procurement inquiries due to their intrinsic endospore structure, which withstands harsh pasteurization, extrusion, and low-pH environment naturally. Formulators are increasingly pairing delicate *Bifidobacteria* strains with resilient *Bacillus* spores to build resilient synbiotic products capable of multi-year shelf stability without specialized cold-chain logistics.
Generic multi-strain probiotics are giving way to clinically backed, target-specific formulations. Procurement preferences have transitioned toward:
Global consumer pressure for eco-friendly packaging is driving Chinese manufacturers to innovate high-barrier compostable sachets. New aluminum-free laminate films offer identical oxygen and water-vapor moisture transmission rates (WVTR $< 0.05 \text{ g/m}^2/\text{day}$), allowing brands to maintain 24-month stability while meeting strict EU plastic reduction mandates.
Direct technical answers addressing critical manufacturing specifications, quality assurance, and contract manufacturing logistics.
Survival is guaranteed through a four-stage preservation protocol: (1) Deep freeze-drying (lyophilization) with specialized protective disaccharides; (2) Microencapsulation of sensitive strains; (3) Strict environmental control keeping water activity ($a_w$) under 0.15; and (4) High-barrier aluminum foil sachet or bottle packaging flushed with dry Nitrogen gas ($O_2 < 1\%$). Furthermore, overage (typically 15%–30% extra CFU at input) is calculated into the formulation to ensure labeled potency at expiration.
Stock formulas are pre-formulated, stability-tested blends (e.g., 50 Billion CFU Daily Gut Health) that allow rapid market launch with MOQs as low as 500 units and lead times of 2–3 weeks. Custom strain development involves tailored strain selection, precise CFU ratio adjustment, custom prebiotic matrix integration, and dedicated stability testing. Custom projects typically carry higher MOQs and require 4–6 weeks for raw material sourcing and pilot validation.
Production is conducted within Class 100,000 cleanroom environments operating under positive pressure. Factories employ segregated blending suites equipped with dedicated dust extraction systems. Between production runs of different microbial strain profiles, automated Clean-In-Place (CIP) and Sterilization-In-Place (SIP) protocols clean all contact surfaces, followed by environmental swab testing to verify zero cross-contamination.
Every shipment includes a comprehensive Certificate of Analysis (CoA) containing: (1) Live Cell Count (CFU/g) via ISO/AOAC flow cytometry methods; (2) Strain identification confirmation via 16S rRNA gene sequencing; (3) Heavy metal testing (Lead, Arsenic, Cadmium, Mercury via ICP-MS); (4) Microbiological safety screening (Salmonella, E. coli, Staphylococcus aureus, Yeast & Mold); and (5) Physical parameters (Water activity $a_w$, bulk density, particle size mesh distribution).
Yes, synbiotic combinations are extremely common. However, raw material compatibility must be scientifically evaluated. Herbal extracts with high hygroscopicity or acidic active ingredients (such as Vitamin C or organic acids) can elevate local water activity or lower pH, harming sensitive *Lactobacillus* cells. Our formulation team performs compatibility pre-screens, utilizing microencapsulated vitamins or granular plant extracts to protect live cultures within the powder matrix.
Standard lead time for stock formulas is 15–21 days post label artwork approval. Custom formulations require 30–45 days to allow for raw material sourcing, strain assay validation, and stability check. Products can be shipped via express air freight (temperature-monitored for high-potency bulk strains) or sea freight utilizing refrigerated reefer containers set at 4°C–15°C to preserve maximum viable counts during transit.
Partner with China's leading cGMP probiotic powder manufacturer. Talk directly with our bioprocess engineers to request custom formulations, request free laboratory samples, or get an instant factory-direct bulk quote.