Explore our CE-compliant, cGMP-produced bulk dietary supplements available for private label OEM/ODM customization with flexible MOQs.
The global dietary supplement industry has entered a new epoch defined by stringent regulatory scrutiny, consumer demand for functional transparency, and complex international compliance benchmarks. As brand owners, pharmaceutical distributors, and retail conglomerates scale their product portfolios, partnering with a fully CE Certified Bulk Supplements Manufacturer is no longer merely a supply-chain option—it is a core risk-mitigation strategy.
Navigating international markets requires adherence to stringent regulatory frameworks including the European Union's General Food Law (Regulation EC 178/2002), Food Information to Consumers (Regulation EU 1169/2011), cGMP (Current Good Manufacturing Practice), HACCP (Hazard Analysis Critical Control Point), and ISO-backed quality systems. Contract manufacturing has evolved from basic ingredient blending to sophisticated bio-engineering, demanding advanced particle micronization, liposomal bioavailability enhancement, stable gummy matrix chemistry, and clean-label botanical extraction.
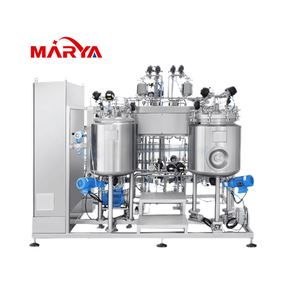
While dietary supplements are legally classified under specialized food safety frameworks in many jurisdictions, CE compliance and European conformity certifications signify that manufacturing facilities operate under validated electrical, mechanical, and bio-process safety controls. Our integration of advanced factory automation systems—such as the Marya Professional Formulation System—ensures zero cross-contamination, automated dosage weight precision within ±0.5%, and complete digital batch traceability from raw botanical import to final sealed packaging.
To support high-growth global wellness brands, our manufacturing ecosystem combines scalable volume capabilities with pharmaceutical-grade quality control systems. Operating out of state-of-the-art cleanroom facilities, we engineer bulk delivery systems spanning two-piece hard shell capsules, micro-encapsulated functional powders, high-purity botanicals, and hydro-colloidal gummy candies.
Utilizing automated dosing cleanroom lines with HEPA HVAC filtration (Class D / ISO 8 cleanroom standard). Automated micro-dosing guarantees consistent active ingredient uniform distribution across 1000kg+ production runs.
Every production batch undergoes raw material identity testing (FTIR), assay verification via High-Performance Liquid Chromatography (HPLC), heavy metal screening via ICP-MS, and complete microbiological verification.
From stock formulation ready-to-label solutions with MOQs starting at 500 units to full custom OEM formulation scale-ups exceeding 1,000,000 capsules daily, our production capacity flexes with market demand.
Complete documentation sets provided for every shipment: Certificate of Analysis (CoA), Safety Data Sheets (SDS), Stability Study Logs, Free Sale Certificates, and Label Compliance Dossiers according to EU Regulation 1169/2011.
| Dosage Delivery Format | Technical Specifications | Quality Assurance Protocols | Primary Regulatory Compliance |
|---|---|---|---|
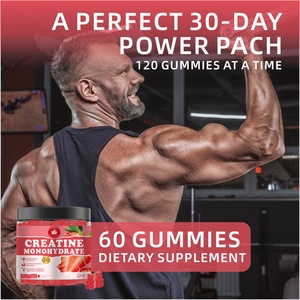
| Creatine & Functional Gummies | Pectin/Gelatin matrix, low-moisture thermal processing, 5g active load capacity without sugar crystallization. | Brix stability check, water activity (aw) < 0.65, texture analysis verification. | CE Equipment Standard, EU Food Grade Pectin, Non-GMO Certified. |
| Vegetable & Gelatin Capsules | Sizes #00, #0, #1; HPMC vegetarian shells, delayed-release gastro-resistant enteric coating options. | Disintegration testing (< 15 mins), weight variation (±3%), lock-length validation. | cGMP, ISO 22000, Halal & Kosher Certificate Validation. |
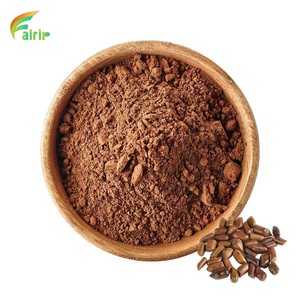
| Bulk Botanical Powders & Extracts | 10:1 to 50:1 standardized extract ratios, spray-dried aqueous/ethanol extractions, high mesh fineness (80-120 mesh). | Marker compound assay (HPLC/UV), pesticide residue screening (LC-MS/MS), solvent residue check. | EU Novel Food Status Verification, Heavy Metal limits (EC 1881/2006). |
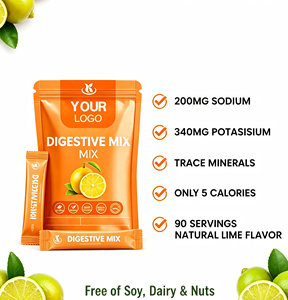
| Electrolyte & Protein Powders | Micro-encapsulated mineral ions, instantized vegan/whey protein isolates, zero-sugar keto formulations. | Particle size distribution, bulk density checks, moisture content (< 5%), solubility speed profiling. | HACCP Food Safety Critical Control Point, Allergen Isolation Control. |
The dietary supplement procurement landscape is undergoing rapid structural transformations. B2B buyers must align their product development pipelines with emerging science, changing regulatory frameworks, and shifting consumer demographics.
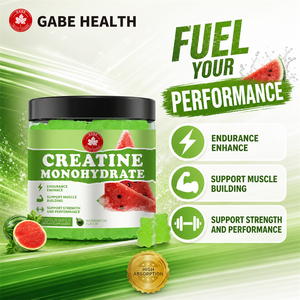
Historically limited to basic multivitamins, gummy confectionery delivery systems are now dominating sports nutrition and cognitive performance categories. The successful formulation of high-dose Creatine Monohydrate Gummies and botanical extracts requires advanced thermal stability controls to preserve thermolabile active compounds during the deposit phase. Traditional tablet pressing is declining due to consumer tablet-fatigue, driving brands toward functional gummies and instant-dissolve sachets.
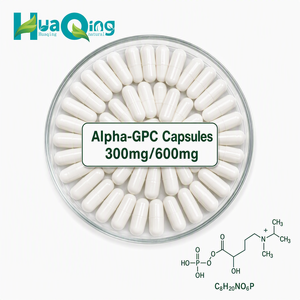
Compounds such as Alpha-GPC (L-Alpha Glycerylphosphorylcholine), Phosphatidylserine, and Lions Mane extract represent the fastest-growing market segments in North America and Europe. Buyers are increasingly specifying high-purity, liposomal, or choline-stabilized formulations to prevent hygroscopic degradation during storage and transit.
Procurement directors are shifting away from generic plant powders toward extract formulations with guaranteed chemical marker levels (e.g., standardized cassia seed extracts, ashwagandha with verified withanolide percentages). Furthermore, synthetic excipients like magnesium stearate and silicon dioxide are being replaced by organic rice hulls and natural acacia fiber to satisfy clean-label guidelines.
Global buyers are prioritizing contract manufacturers that provide verifiable sustainability data. From solar-assisted manufacturing cleanrooms to zero-waste packaging materials and ethically harvested botanicals, ESG metrics have become explicit evaluation criteria in enterprise B2B vendor audits.
Achieving peak efficacy in bulk dietary supplements requires meticulous physical and chemical optimization during R&D. Below is an analytical review of key formula architectures produced within our CE-certified facility:
Creatine monohydrate remains the gold standard in cellular hydration and ATP regeneration. However, traditional powders often suffer from poor solubility. Our factory utilizes 200-mesh ultra-micronization, alongside high-stability pectin gummy encapsulation that protects the creatine compound from premature degradation into creatinine in low pH environments.
Modern hydration science balances sodium, potassium, magnesium glycinate, and trace ionic minerals without heavy sugar bases. Our low-carb electrolyte powder blends feature micro-encapsulated mineral salts to neutralize harsh metallic tastes, combined with natural fruit acid profiles for rapid osmolality absorption.
Below are expert responses to essential operational, technical, and regulatory questions encountered by enterprise buyers when sourcing custom OEM/ODM bulk supplements.
Our manufacturing infrastructure adheres to strict cGMP guidelines, ISO 22000 food safety standards, and HACCP control protocols. For European distribution, all product formulations are screened to guarantee compliance with EU Regulation (EC) No 178/2002 (General Food Law), Regulation (EC) 1881/2006 (setting maximum levels for contaminants), and Regulation (EU) 1169/2011 for accurate labeling declarations. Additionally, equipment holds CE certification, confirming adherence to structural, mechanical, and environmental health standards.
The Marya system is an integrated cleanroom automation architecture engineered for ultra-precise powder blending, moisture control, and automatic capsule filling. By eliminating manual powder handling, it prevents cross-contamination, regulates ambient cleanroom humidity (preventing hygroscopic active ingredients like Alpha-GPC from clumping), and guarantees fill weight tolerances within ±0.5% variance.
To accommodate scaling brands, ready-to-brand stock formulations (such as standard Creatine Monohydrate Powders or Botanical Extracts) start at low minimums of 500 units per SKU. Custom OEM formulations involving specialized active combinations, custom gummy molds, or bespoke flavoring systems typically start at 3,000 to 5,000 units, depending on raw material sourcing parameters.
Every dispatched shipment includes a comprehensive Certificate of Analysis (CoA) verified by independent or internal laboratory testing. The CoA verifies active constituent potency via HPLC/UV, verifies heavy metal compliance (Lead, Cadmium, Mercury, Arsenic via ICP-MS), confirms microbiology limits (Total Plate Count, Yeast & Mold, E. coli, Salmonella), and records physical parameters such as disintegration times and moisture content.
Yes. We specialize in complex delivery formats. Our pectin-based gummy line is tailored to incorporate high active loads (such as 1000mg+ of active creatine per serving) without compromising physical texture or taste stability. For nootropics like Alpha-GPC, we utilize vegetable HPMC shells with desiccated packaging protocols to guarantee shelf-life stability against moisture degradation.
For stock formulations with existing labels, lead times are approximately 2 to 3 weeks. For custom OEM projects requiring lab sample approval, flavoring adjustment, stability testing, and packaging printing, standard lead times range from 4 to 6 weeks following sample sign-off.
Our structured six-stage manufacturing methodology guarantees complete operational alignment between product inception and retail delivery:
Defining dosage specs, active target potency, packaging aesthetics, target pricing, and destination market regulatory requirements.
Formulating pilot lab batches for physical texture analysis, solubility checks, organoleptic testing, and active stability confirmation.
Procuring certified, high-purity raw ingredients from validated vendors with strict identity, purity, and non-GMO documentation.
Executing automated blending, micro-dosing, capsule filling, or gummy cooking using the automated Marya manufacturing line.
Performing HPLC assays, microbial cultures, and heavy metal sweeps to generate validated certificates of analysis per batch.
Executing primary bottling/sachet sealing, secondary carton assembly, pallet wrapping, and dispatch with complete customs clearance documentation.
Whether you are expanding an established brand or launching a innovative custom formulation, our engineering team is ready to scale your production with uncompromised quality, regulatory compliance, and rapid market turnaround.